 EN
How to Vet a Fiberglass Tube Manufacturer Without Getting Burned
I've Been Burned by the Wrong Fiberglass Tube Manufacturer — Twice
I've been in composites since 1989. I've bought fiberglass tube from suppliers in five countries. I've also sent two truckloads of reject tube back to a fiberglass tube manufacturer in 2003 and paid the freight on both loads. That little education cost me about forty thousand dollars and a client I never won back.
Most procurement teams vet a supplier the same way they pick paper. They scan the website. They collect three quotes. They sign with whoever lands in the middle. That works fine for copy paper. It gets somebody hurt when the tube is carrying load or sitting in a corrosive ditch.
The gap between a competent fiberglass tube manufacturer and a sloppy one is never on the data sheet. It shows up on the floor. Check the resin drum. See whether the operator running the pultrusion line can read an exotherm before it runs away on him. I'm going to walk you through how I screen suppliers now, after thirty-five years of paying tuition to this industry.
The Resin System Tells You Everything
Ask the fiberglass tube manufacturer what resin they run for your application. Then shut up and listen.
If the answer is "iso resin" and nothing else, leave. If they can name the brand, quote the styrene content, explain why they switched from a bisphenol-A vinyl ester to a novolac epoxy vinyl ester for your temperature range, sit down. You're talking to someone who actually formulates. That's the person you want building your tube.
I walked a plant in Jiangsu in 2011. They were running pultruded tube for a cooling tower project. Beautiful operation. Clean creels. The line supervisor told me the exact MEKP percentage he was pushing and why he'd backed it off half a point when the shop temperature climbed in summer. That's a shop that controls its process. We bought from them for nine years.
Resin choice decides whether your tube survives ten years in a scrubber or fails in eighteen months. A polyester pultruded tube is cheap. It's also wrong for anything carrying acidic condensate. A proper vinyl ester tube costs more. It also doesn't crack along the glass when the temperature spikes. If the supplier can't explain that tradeoff in plain language, they're buying resin by the drum and hoping for the best.
Walk the Floor or Don't Sign the Contract
I do not buy structural tube from a fiberglass tube manufacturer I have not walked through. Period.
You can tell more in twenty minutes on the floor than in twenty hours of email. Look at the roving creels. Are they clean? Is there broken strand piled up under the guides? A shop that lets waste accumulate under the forming box is a shop that lets defects accumulate in the wall. Look at the resin bath. Is the level consistent? Is the temperature controlled? Resin viscosity changes with temperature. Wet-out changes with viscosity. Glass content changes with wet-out. A manufacturer that doesn't control bath temperature doesn't control what's in the tube. That's not opinion. That's physics.
I visited a fiberglass tube manufacturer in 2016 that ran a beautiful-looking filament winding line. Spotless floor. New equipment. The sales guy was sharp. But the cure oven had a cold zone the operator didn't know about. I caught it because I ran my hand along a finished tube and felt a soft spot three meters in. Green strength was there but the back half of the part was undercured. They'd been shipping that tube for a year. Nobody had complained yet. Somebody would have.
We didn't buy from them. The competitor two provinces over had an older line but a cure schedule printed and taped to the control panel, with oven temperatures logged every shift. Old equipment run by people who care beats new equipment run by people who don't. Every single time.
Spec Sheets Lie. Barcol Readings Don't.
Every fiberglass tube manufacturer hands you a spec sheet. They all look the same. Tensile strength, flexural modulus, glass content, Barcol hardness, all in neat columns.
Half of them are copied from a competitor's website. I've caught that twice.
The spec sheet tells you what the material is supposed to do. It does not tell you what shipped on the truck. The only way to know what shipped is to test it. Barcol hardness is the cheapest, fastest indicator you have. A Barcol 934-1 impressor runs about three hundred dollars. It tells you in five seconds whether the tube is cured. Undercured tube reads low. Undercured tube creeps under load. Undercured tube fails in service.
I make every new fiberglass tube manufacturer send a sample before the first production order. I put a Barcol on it. I burn a small piece and look at the ash. If the glass content looks off, I send it to a lab for ignition loss. That costs me about eighty dollars and a week. It has saved me from two bad suppliers.
One supplier in 2019 sent me tube that read Barcol 38 on a spec that called for 45 minimum. I called them. They said it was within tolerance. Tolerance was plus or minus five. Thirty-eight is not within tolerance of forty-five. They argued. I hung up. That's a fiberglass tube manufacturer that either doesn't test or doesn't care. Either way, I was done.
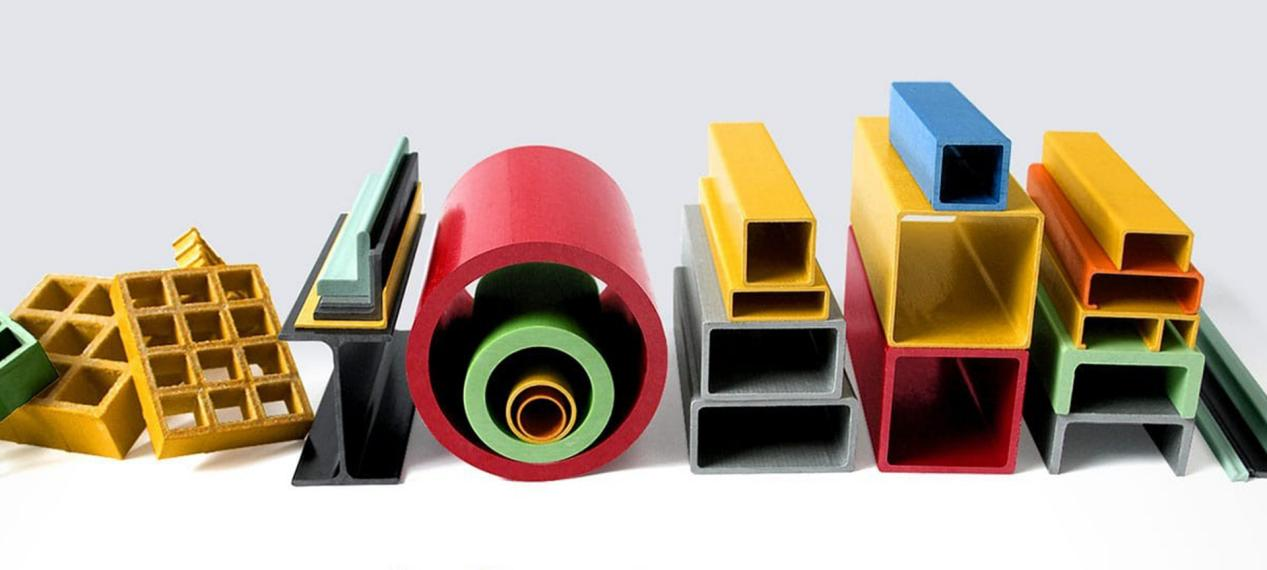
The Green Strength Problem Nobody Talks About
Here's something most buyers never think about. Fiberglass tube has green strength. That's the strength the part holds right out of the die, before it's fully post-cured. A good shop manages green strength because it's what gets the tube through cutoff and handling without cracking.
A bad one ignores it. The tube comes off the line soft. It gets cut. It gets stacked. It deforms under its own weight in the rack. By the time it reaches you, it looks fine but the wall has internal microcracks you can't see. Those cracks open up under pressure cycling. That's how a tube that passed incoming inspection fails six months into service.
I learned this in 2006. We had a batch of pultruded tube crack along a spiral line in a structural application. The investigation took three months. Root cause was green strength too low at cutoff, combined with a puller speed that was too fast for the die temperature. The fiberglass tube manufacturer had bumped line speed to hit a delivery date. Nobody told us. The tube passed every test we ran on receipt. It failed in the field.
Ask your supplier about pull speed and die temperature. If they can't answer, they don't control the variable that matters most.
Price Gaps That Actually Mean Something
A fiberglass tube manufacturer quoting thirty percent under the market is not giving you a deal. They're cutting something.
I've seen it all. Lower glass content. Cheaper resin. Thinner wall. Skipped post-cure. The cheapest quote I ever took was from a supplier in 2014. The tube looked identical to the spec. Same OD. Same color. Same wall thickness on the caliper. The resin was ortho polyester relabeled as iso. The glass content was four percent low. The tube failed hydrostatic testing at sixty percent of rated pressure.
Standard pultruded vinyl ester tube runs in a predictable band. I'm not going to quote you today's number because resin pricing moves. But when one fiberglass tube manufacturer comes in twenty-five percent below the pack, something is missing from the wall or the resin or the cure. Pay the fair price. The money you save on the front end you spend five times over on field failures, expedited replacements, and the conversation where you explain to your boss why the project is delayed.
The Acceptance Test Most Buyers Skip
Most buyers do incoming inspection on dimensions. OD, wall thickness, length, straightness. That's it.
That's not enough. Dimensional inspection catches the tube that's the wrong size. It does not catch the tube that's the right size and the wrong material.
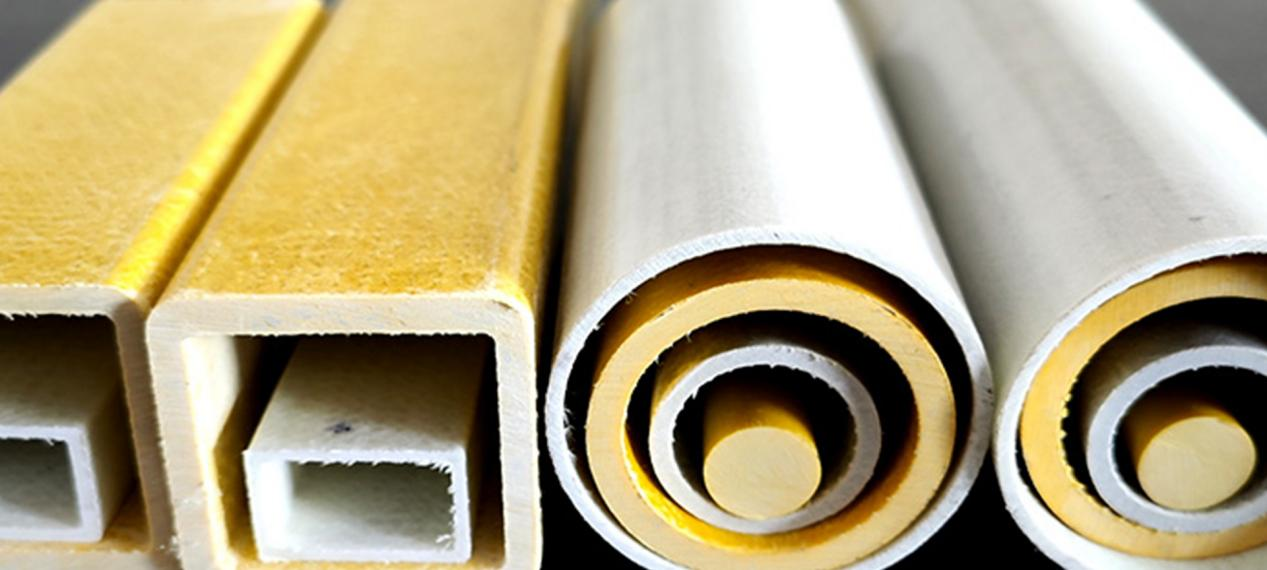
I run three tests on every new supplier's first shipment. Barcol hardness for cure. Ignition loss for glass content. And a visual on the cut end under a ten-power loupe for voids and dry spots. Dry glass in the wall means wet-out was poor. Voids mean the resin bath was starved or the vacuum was off. A shop with good process control produces a cut end that looks like solid material. A bad one produces a cut end that looks like fiberglass insulation with some resin dribbled in.
The loupe cost me twelve dollars. It has rejected more tube than any other tool in my kit.
What I Demand From a Supplier Now
I've boiled my requirements down over thirty-five years. A fiberglass tube manufacturer earns my order when they can do four things.
Tell me the resin system by name and why they picked it. Let me walk the floor without a handler steering me away from the cure oven. Send a sample that passes my Barcol and my loupe before the first production run. And log their pull speed and die temperature every shift, on paper I can read.
That's it. Four things. Most shops can't do all four. The ones that can are worth whatever they charge, because the alternative is the phone call at two in the morning telling you a tube failed and a system is down.
I've taken that call. I don't take it anymore. Vet your fiberglass tube manufacturer like your project depends on it. It does.